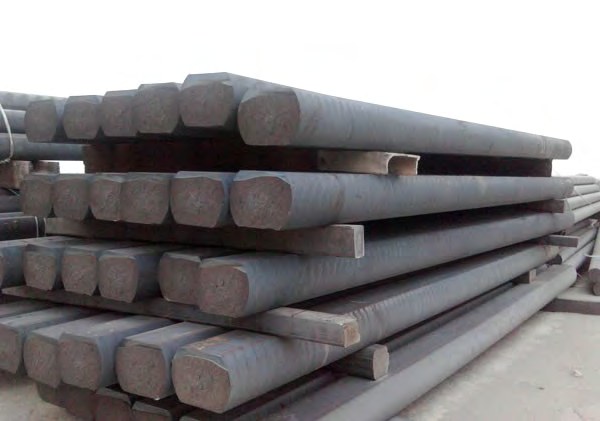
Gray iron and ductile iron have almost the same chemistry. What separates them is the shape the carbon takes when the iron solidifies: interconnected graphite flakes in gray iron, isolated graphite spheres in ductile iron.
Flakes act as internal notches. They cut the effective load-bearing section and give gray iron its low tensile strength and near-zero elongation — but they also give it outstanding vibration damping, thermal conductivity and self-lubricating sliding behaviour.
Nodules do not act as notches. Ductile iron therefore keeps most of the machinability advantage of cast iron while reaching strength and elongation figures comparable with medium-carbon steel.
Mechanical properties side by side
| Grade | Type | Yield (MPa) | Tensile (MPa) | Hardness (HB) | Elongation (%) |
|---|---|---|---|---|---|
| HT200 | Gray | ≥120 | ≥180 | 150–180 | — |
| HT250 | Gray | ≥150 | ≥220 | 170–220 | — |
| HT300 | Gray | ≥180 | ≥260 | 190–240 | — |
| QT400-18 | Ductile | ≥260 | ≥380 | 130–170 | ≥18 |
| QT450-10 | Ductile | ≥310 | ≥420 | 140–200 | ≥12 |
| QT500-7 | Ductile | ≥320 | ≥470 | 150–230 | ≥7 |
| QT600-3 | Ductile | ≥380 | ≥560 | 180–250 | ≥3 |
Mechanical properties of continuous cast gray and ductile grades
Values are for sections Φ30–150 mm; larger diameters carry slightly lower minima. Properties are measured at 1/4 diameter (round) or 1/4 diagonal (square and rectangle).
Chemistry
| Element | Gray HT200–HT300 | Ductile QT400-18–QT600-3 |
|---|---|---|
| C | 2.8–3.8 | 3.0–4.0 |
| Si | 2.0–2.8 | 2.0–3.2 |
| Mn | 0.3–1.2 | 0.1–0.8 |
| P | ≤0.15 | ≤0.10 |
| S | ≤0.10–0.12 | ≤0.02–0.03 |
Typical composition ranges (%)
The tight sulphur ceiling on ductile grades is what allows magnesium treatment to nodularise the graphite; high sulphur consumes magnesium and leaves degenerate structures.
International equivalents
| China (GB) | U.S.A. (ASTM) | E.U. (EN) | Germany (DIN) | Japan (JIS) |
|---|---|---|---|---|
| HT200 | No. 30 | EN-GJL-200 | GG20 | FC200 |
| HT250 | No. 35 | EN-GJL-250 | GG25 | FC250 |
| HT300 | No. 45 | EN-GJL-300 | GG30 | FC300 |
| QT400-18 | 60-40-18 | EN-GJS-400-18 | GGG40 | FCD400 |
| QT450-10 | 65-45-12 | EN-GJS-450-10 | GGG45 | FCD450 |
| QT500-7 | 70-50-05 | EN-GJS-500-7 | GGG50 | FCD500 |
| QT600-3 | 80-55-06 | EN-GJS-600-3 | GGG60 | FCD600 |
Core continuous cast grades and international equivalents
How to choose
Choose gray iron when
- Vibration damping matters — machine tool bases, mould plates, press beds, guide surfaces.
- Sliding wear against another metal surface is the duty cycle, and the graphite acts as a lubricant reservoir.
- Thermal conductivity matters — brake, clutch and heat-transfer components.
- Loading is compressive and elongation is not a design requirement.
- The lowest machining cost per part is the priority.
Choose ductile iron when
- The part sees tensile, bending or impact loading — shafts, levers, brackets, hydraulic bodies.
- You need elongation and toughness, not just compressive strength.
- The alternative under consideration is 45# or C45 medium-carbon steel.
- Pressure tightness is required, which the dense nodular structure delivers without impregnation.
- Weight reduction through higher allowable stress is worthwhile.
- Graphite shape, not chemistry, is the defining difference: flakes in gray iron, nodules in ductile iron.
- Gray grades HT200–HT300 deliver 180–260 MPa tensile with no usable elongation but excellent damping and sliding wear behaviour.
- Ductile grades QT400-18–QT600-3 deliver 380–560 MPa tensile with 3–18% elongation.
- Ductile iron requires low sulphur (≤0.02–0.03%) so magnesium treatment can nodularise the graphite.
- Choose gray for damping, wear and compression; choose ductile for tension, impact and pressure tightness.